Sponsored article
Why Do Bioplastics and Recycled Plastics Require a Different Approach in the Production of Bar Trays and POS Materials?
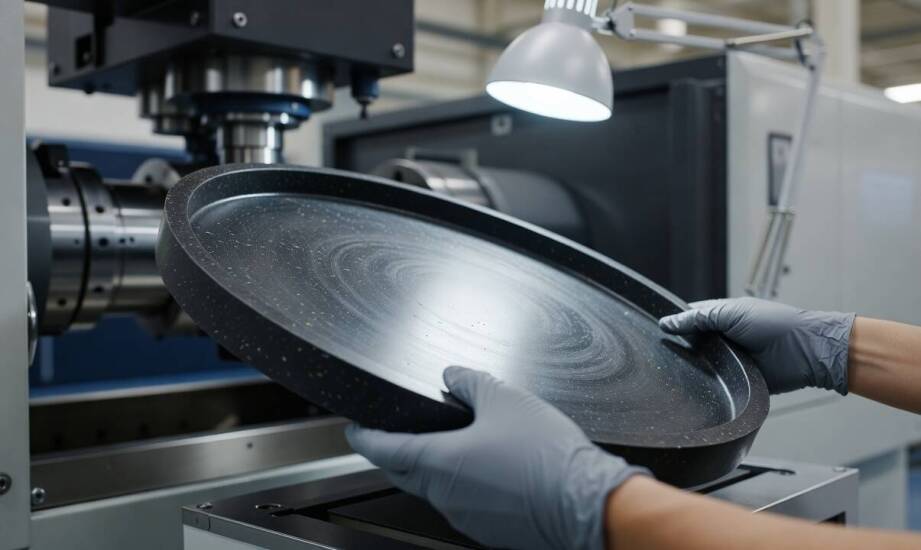
Introducing bioplastics or recycled plastics into high-volume production requires a careful analysis of injection moulding parameters.
Read more: Differentiation of the wholesale mushroom offering as support for culinary creativity
Replacing a conventional polymer with an alternative material can significantly change melt flow, shrinkage, thermal behaviour and processing stability, which means that the production process may need to be adjusted rather than simply run with the same settings.
Customers in the catering, pharmaceutical and advertising sectors increasingly take environmental considerations into account when selecting new products. At the same time, they continue to expect suitable mechanical strength, repeatability and appearance.
Bar trays, display components and point-of-sale materials must therefore combine the intended environmental properties with the performance required in everyday use.
Successful implementation depends on selecting the right polymer grade and matching the injection moulding process to its actual characteristics. The final result is determined by materials engineering and process control, not by environmental claims alone.
How Do Viscosity and Shrinkage Affect Injection Moulding?
The rheological behaviour of bioplastics and recycled polymers can differ from that of conventional virgin materials.
Differences in melt viscosity may require changes to injection pressure, temperature profile and injection speed.
Materials such as polylactic acid (PLA) or polyhydroxyalkanoates (PHA), for example, can have processing windows that differ considerably from those of commonly used conventional polymers.
Their behaviour depends on factors including:
polymer grade,
moisture content,
melt temperature,
shear rate,
residence time,
part geometry.
If the material does not flow sufficiently well, it may fail to fill thin sections or more distant areas of the cavity.
Increasing the temperature is not always the correct solution. Excessive processing temperatures or residence times can cause polymer degradation, reducing the quality of the finished part.
Flash formation, on the other hand, may result from a combination of reduced melt viscosity, excessive pressure, insufficient clamping or problems with the moulding tool. It should therefore not be attributed to thermal degradation alone.
Shrinkage is another important factor.
Changes in shrinkage behaviour can affect dimensional stability, particularly in large, flat or geometrically complex parts.
This is relevant for POS components that need to fit precisely into dispensers, stands or modular display systems.
Cooling time, holding pressure, wall thickness and part geometry all influence the final dimensions.
Recycled materials can also show greater batch-to-batch variability depending on the source, composition and level of contamination or blending. This makes incoming material control particularly important.
Why May the Mould Need to Be Adapted?
Changing the polymer does not always require a completely new mould, but it may require adjustments to the tool or process parameters.
The gating system, venting, cooling circuit and ejection system should be evaluated against the characteristics of the new material.
A mould originally designed for polypropylene, for example, may not automatically provide optimum results when used with a different biopolymer or recycled compound.
Important factors include:
melt flow behaviour,
processing temperature,
shrinkage,
tendency to warp,
venting requirements,
mechanical properties during ejection.
The layout of ejector pins and the quality of cavity venting can have a significant influence on surface quality and part release.
The appropriate solution therefore depends on the specific material and component rather than on whether the polymer is simply described as “bio-based” or “recycled”.
How Should the Properties of Alternative Materials Be Verified?
The suitability of a material must be assessed in relation to the actual conditions in which the finished product will be used.
For bar trays and POS components, important properties may include:
moisture resistance,
resistance to alcohol or grease,
dimensional stability,
impact resistance,
scratch resistance,
colour stability,
UV resistance where relevant.
Some bio-based or biodegradable materials may be more sensitive to moisture than conventional polymers. However, this varies widely between material families and formulations, so no general conclusion should be drawn solely from the term “bioplastic”.
The same applies to recycled plastics.
Their properties depend on the polymer type, the quality of the recyclate, contamination level, additives and the consistency of the feedstock.
For this reason, quality control should focus on the actual technical specification of the material, rather than only its recycled content.
Noex states that it tests raw materials, materials used in production, components and finished products as part of its manufacturing process.
This type of verification is particularly important when a new material is introduced into serial production.
Standards and Certification
Designing ECO plastic products requires a distinction between different environmental characteristics of materials.
NOEX itself describes its ECO-LINE as including products made using bio-plastics, compostable materials, recycled raw materials and recyclable materials.
These terms should not be treated as interchangeable.
A material can be:
bio-based without being biodegradable,
biodegradable without being suitable for industrial composting,
recycled without being compostable,
recyclable without containing recycled content.
The same distinction applies to certification schemes.
ISCC PLUS is a voluntary certification system for alternative feedstocks and their traceability through the supply chain. It can use several chain-of-custody approaches, including physical segregation, controlled blending and mass balance.
Under the mass balance approach, certified and non-certified materials may be physically mixed while the certified input and its sustainability characteristics are tracked through documented accounting rules.
It should therefore not be described simply as proof that a specific finished item physically contains a stated percentage of recycled material.
EN 13432, meanwhile, concerns packaging recoverable through composting and biodegradation and defines testing and evaluation criteria for such packaging.
It is therefore relevant where a packaging product is intended to meet industrial compostability requirements, but it is not a universal environmental certification for all plastic products.
Keeping these concepts separate helps prevent misleading environmental claims and makes product documentation easier to interpret.
Why Process Stability Matters in High-Volume Production
Large-scale B2B production of injection-moulded components depends on the repeatability of both the material and the process.
Appearance, ergonomics and environmental positioning must be combined with appropriate:
impact resistance,
dimensional stability,
surface quality,
processing repeatability,
long-term suitability for the intended application.
Introducing recycled or bio-based materials therefore often requires additional process validation rather than simply replacing one polymer with another.
Mould design may need to account for different shrinkage or flow behaviour, while injection parameters should be verified under production conditions.
The aim is not to maximise recycled or bio-based content at any cost, but to achieve a technically stable product that meets both functional and environmental requirements.
Key Points About Bioplastics and Recycled Plastics in Injection Moulding
Bioplastics and recycled polymers can behave differently from conventional virgin materials during injection moulding.
Melt viscosity, shrinkage, moisture sensitivity and thermal stability should be assessed for the specific polymer grade.
Introducing a new material may require changes to pressure, temperature, holding time, cooling or even parts of the mould design.
Recycled materials may require additional incoming-material control because their properties can vary between batches.
Environmental terms such as bio-based, biodegradable, compostable, recycled and recyclable describe different characteristics and should not be used interchangeably.
Certification should be interpreted according to its actual scope rather than used as a general environmental claim.
You might be interested

Differentiation of the wholesale mushroom offering as support for culinary creativity
How to Choose the Right Diameter for a Ceramic Breakfast Plate
What to look for when choosing a store offering polish vestments?